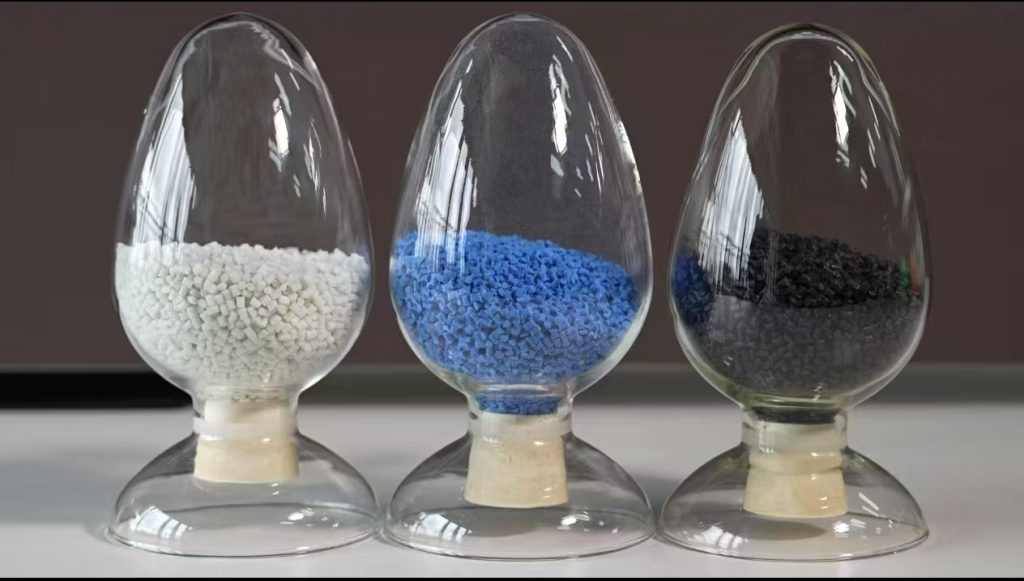
PA6 GF30 is Nylon 6 reinforced with a nominal 30% glass fiber by weight. It is selected when unfilled PA6 does not provide enough stiffness, creep resistance or dimensional stability. This guide combines a real commercial-grade datasheet, typical cross-supplier property ranges, moisture effects and injection-molding starting conditions.
PA6 GF30 at a Glance
The example values below come from the downloadable PA6 WHG30A datasheet. That PDF does not state specimen conditioning; confirm the method and validate molded parts before design approval.
What Does PA6 GF30 Mean?
- PA6 identifies Polyamide 6, also called Nylon 6.
- GF identifies glass-fiber reinforcement.
- 30 identifies the nominal glass-fiber content by weight.
PA6 GF30 is a material family, not one universal recipe. Heat stabilizers, impact modifiers, lubricants, pigments, flame retardants, resin viscosity and fiber system can all change the final properties and molding behavior. Two materials marked PA6 GF30 are therefore not automatically interchangeable.
PA6 WHG30A Manufacturer Datasheet
The downloadable manufacturer TDS identifies the commercial grade as PA6 WHG30A. The following values are reproduced from that one-page document. They are typical product values, not guaranteed design limits.
| Propiedad | Norma de ensayo | Unidad | PA6 WHG30A |
|---|---|---|---|
| Resistencia a la tracción | ISO 527-2 | MPa | 165 |
| Tensile Strain at Break | ISO 527-2 | % | 9 |
| Resistencia a la flexión | ISO 527-2 | MPa | 230 |
| Módulo de flexión | ISO 178 | MPa | 6000 |
| Izod Notched Impact Strength | ISO 179 | kJ/m² | 17 |
| Temperature of Deflection Under Load | ISO 75-2/B | °C | 175 |
| Melting Index | ISO 1183 | g/10 min | 20 |
| Densidad | ISO 1183 | g/cm³ | 1.36 |
| Molding Shrinkage | ISO 2577 | % | 0.6 |
| Inflamabilidad | UL 94 | - | - |
Read the test conditions: ISO 75-2/B is the 0.45 MPa HDT method; it cannot be compared directly with the 1.8 MPa ranges below. The PDF does not state specimen conditioning. Its impact row names Izod but cites ISO 179 (Charpy), its flexural-strength row cites the tensile standard ISO 527-2, and its melting-index row cites ISO 1183 (density); confirm those methods with the supplier before using the figures for approval. The UL 94 result is blank. Request the current signed TDS, batch certificate of analysis and applicable RoHS, REACH or UL documents for the selected grade.
Download PA6 WHG30A Datasheet (PDF)
Need the compound rather than only the data? See the Página del producto PA6 GF30 for grade selection and send the part requirements with your datasheet or sample request.
PA6 GF30 Typical Property Data
The following tables show illustrative ranges across commercial PA6 GF30 formulations, not additional specifications for WHG30A. Use them only to identify questions for grade selection; values can differ with formulation, specimen thickness, method and conditioning. The WHG30A PDF above is the source for that named grade.
Illustrative PA6 GF30 Mechanical Ranges (Dry as Molded Examples)
| Propiedad | Valor (rango típico) | Método de ensayo | Unidad |
|---|---|---|---|
| Módulo de elasticidad | 9,500-10,500 | ISO 527-1/-2 | MPa |
| Resistencia a la tracción en la rotura | 170-190 | ISO 527-1/-2 | MPa |
| Alargamiento a la rotura | 3.0-4.5 | ISO 527-1/-2 | % |
| Módulo de flexión | 8,000-9,500 | ISO 178 | MPa |
| Resistencia a la flexión | 260-290 | ISO 178 | MPa |
| Resistencia al impacto según el método Charpy (con muesca) | 12-16 | ISO 179/1eA | kJ/m² |
| Resistencia al impacto según el método Charpy (sin muesca) | 75-95 | ISO 179/1eU | kJ/m² |
| Resistencia al impacto Izod (con muesca) | 11-15 | ISO 180/A | kJ/m² |
| Dureza por indentación con bola | 200-230 | ISO 2039-1 | MPa |
Propiedades físicas
| Propiedad | Valor (rango típico) | Método de ensayo | Unidad |
|---|---|---|---|
| Densidad | 1.35-1.38 | ISO 1183 | g/cm³ |
| Absorción de agua (23 °C, saturación) | 5.5-6.5 | ISO 62 | % |
| Absorción de agua (23 °C, equilibrio de humedad relativa 50%) | 1.5-2.0 | ISO 62 | % |
| Contracción por moldeo (paralela, 1,6 mm) | 0.25-0.40 | ISO 294-4 | % |
| Contracción por moldeo (normal, 1,6 mm) | 0.80-1.10 | ISO 294-4 | % |
| Contracción tras el moldeo (paralela, 1 h a 110 °C) | 0.05-0.10 | ISO 294-4 | % |
| Contracción tras el moldeo (normal, 1 h a 110 °C) | 0.10-0.15 | ISO 294-4 | % |
Propiedades térmicas
| Propiedad | Valor (rango típico) | Método de ensayo | Unidad |
|---|---|---|---|
| Temperatura de fusión (DSC, 10 K/min) | 218-222 | ISO 11357-1/-3 | C |
| HDT a 0,45 MPa | 215-220 | ISO 75-1/-2 | C |
| HDT a 1,8 MPa | 195-210 | ISO 75-1/-2 | C |
| Temperatura de reblandecimiento Vicat (VST/B50) | 205-215 | ISO 306 | C |
| Coeficiente de expansión térmica lineal (paralelo, 23-55 °C) | 2.0-3.0 x 10⁻⁵ | ISO 11359-1/-2 | 1/K |
| Coeficiente de expansión térmica lineal (normal, 23-55 °C) | 6.0-9.0 x 10⁻⁵ | ISO 11359-1/-2 | 1/K |
| Conductividad térmica | 0.28-0.35 | DIN 52612 | W/(m·K) |
| Capacidad calorífica específica | 1.5-1.7 | — | J/(g·K) |
Propiedades eléctricas
| Propiedad | Valor (rango típico) | Método de ensayo | Unidad |
|---|---|---|---|
| Constante dieléctrica (1 MHz) | 3.5-4.5 | IEC 60250 | — |
| Factor de disipación (1 MHz) | 0.01-0.03 | IEC 60250 | — |
| Resistividad volumétrica | 1013-1015 | IEC 60093 | ohm·cm |
| Resistividad superficial | 1012-1014 | IEC 60093 | ohm |
| Índice de Seguimiento Comparativo (ISC) | 500-600 | IEC 60112 | V |
| Rigidez dieléctrica (1,6 mm) | 30-35 | IEC 60243-1 | kV/mm |
Inflamabilidad
| Propiedad | Valor | Método de ensayo | Notas |
|---|---|---|---|
| Clasificación UL 94 (0,8 mm) | HB | UL 94 | El modelo GF30 estándar no es ignífugo |
| Clasificación UL 94 (1,6 mm) | HB | UL 94 | La norma FR V-0 exige un compuesto ignífugo especializado |
| Índice de límite de oxígeno (LOI) | 22-24% | ISO 4589 | Arde en condiciones atmosféricas normales |
| Temperatura de autoignición | >400 °C | ASTM D1929 | — |
Cambios en las propiedades con el control de la humedad
El PA6 absorbe humedad del ambiente. En condiciones de equilibrio con una humedad relativa de 50% a 23 °C, una pieza de PA6 GF30 absorberá aproximadamente entre 1,5 y 2,0% de agua en peso. Esto altera significativamente las propiedades mecánicas. La resistencia a la tracción disminuye entre un 30 y un 40%, el módulo de flexión entre un 25 y un 35%, y la resistencia al impacto aumenta entre un 50 y un 100%. La tabla de datos que figura a continuación muestra la variación aproximada entre los valores «en seco, tal y como se ha moldeado» y los valores «acondicionados» (50% de humedad relativa):
| Propiedad | En seco (tal y como se ha moldeado) | En condiciones controladas (50% RH, 23 °C) | Cambiar |
|---|---|---|---|
| Resistencia a la tracción (MPa) | 180 | 110-130 | de -30 a -40% |
| Módulo de flexión (GPa) | 9.0 | 6.0-7.0 | de -25 a -35% |
| Resistencia al impacto con muesca según Charpy (kJ/m²) | 14 | 20-28 | +50 a +100% |
| HDT at 1.8 MPa (C) | 200 | 65-75 (wet) | Significant drop at full saturation |

Parámetros de procesamiento
Secado
El PA6 GF30 debe secarse hasta alcanzar un contenido de humedad inferior a 0,101 TP3T (objetivo: 0,051 TP3T) antes del moldeo por inyección. Secado recomendado: 80 °C durante 4-6 horas en un secador desecante con un punto de rocío de -30 °C o inferior. El secado en bandejas a 80 °C durante 8-12 horas es aceptable para aplicaciones no críticas, pero resulta menos fiable que el secado con desecante. No se debe secar a temperaturas superiores a 90 °C, ya que a temperaturas más altas comienza la decoloración oxidativa (amarilleamiento).
Moldeo por inyección
| Parámetro | Rango recomendado | Notas |
|---|---|---|
| Temperatura de fusión (boquilla) | 250-280 °C | El extremo inferior para paredes finas, el superior para paredes gruesas |
| Temperatura del molde | 80-100 °C | Se recomienda una temperatura de 100 °C para mejorar la cristalinidad y la superficie |
| Velocidad de inyección | De medio a rápido | Un llenado más rápido reduce la variación en la orientación de las fibras |
| Mantener la presión | 50-80% de presión de inyección | Lo suficiente para compensar la contracción y evitar el sobreembalaje |
| Contrapresión | 5-15 bar (hidráulico) | Una mayor contrapresión mejora la homogeneidad de la masa fundida |
| Velocidad del tornillo | 50-150 rpm | Extremo inferior para granallados de mayor tamaño, con el fin de evitar el calentamiento por cizallamiento |
| Tiempo de permanencia (máximo a la temperatura de fusión) | 10-15 minutos | Purgar si el tiempo es mayor; el PA6 degradado produce marcas de quemaduras y pérdida de resistencia |
Aspectos a tener en cuenta en el diseño de moldes
- Tipo de compuerta: Son aptos todos los tipos de boquilla estándar. Las boquillas de pasador, las de borde y las de abanico funcionan bien. En el caso de las boquillas de túnel (submarinas), hay que prestar atención al diámetro de la boquilla: debe ser de al menos 0,8 mm para evitar un cizallamiento excesivo con el 30% GF.
- Ubicación de la puerta: Coloca la entrada de material de manera que el flujo se dirija hacia la sección más gruesa. Evita los recorridos largos que permitan que el frente de material fundido se enfríe antes de que se llene la cavidad.
- Desahogo: Es fundamental que la ventilación sea adecuada. Una ventilación deficiente provoca marcas de quemadura, piezas incompletas y acumulación de material en el troquel. Profundidad de la ventilación: 0,01-0,02 mm.
- Ángulo de calado: Mínimo 1 grado; se recomienda 2 grados para superficies texturizadas. Los grados GF se contraen firmemente sobre los núcleos; un ángulo de desmoldeo adecuado evita daños durante la expulsión.
- Selección del acero: La fibra de vidrio 30% es abrasiva. Para series de producción que superen las 100 000 inyecciones, utilice acero para herramientas endurecido (mín. 52 HRC) para las cavidades y los núcleos, especialmente en los puntos de inyección y en las zonas de mayor desgaste.
Comparing PA6 GF30 with Related Grades
PA6 GF30 is a common selection, but the following cross-grade values are screening examples, not a matched set of supplier specifications. Compare test method, load and conditioning before using them in a design decision. See the PA6 GF15, PA6 GF30 y PA6 GF40 pages for the available grade routes.
| Propiedad | PA6 sin relleno | PA6 GF15 | PA6 GF30 | PA6 GF50 | PA66 GF30 |
|---|---|---|---|---|---|
| Resistencia a la tracción (MPa) | 80 | 120-140 | 170-190 | 200-230 | 180-200 |
| Módulo de flexión (GPa) | 2.8 | 5.5-6.5 | 8.0-9.5 | 14-16 | 9.0-10.5 |
| Resistencia al impacto Izod con muesca (kJ/m²) | 5-7 | 7-10 | 11-15 | 13-18 | 10-13 |
| HDT at 1.8 MPa (C) | 65-75 | 180-195 | 195-210 | 210-215 | 240-255 |
| Densidad (g/cm³) | 1.14 | 1.23 | 1.36 | 1.56 | 1.37 |
| Coste relativo | 1.0x | 1.1x | 1.2x | 1.4x | 1.3x |
PA6 Glass Fiber Grade Comparison: GF15 vs GF30 vs GF40 vs GF50
Glass fiber content drives the performance-cost trade-off in PA6 compounds. The table below shows how increasing glass fiber from 15% to 50% changes key mechanical and thermal properties. Use these screening values to narrow your grade selection before requesting commercial datasheets.
| Propiedad | PA6 sin relleno | PA6 GF15 | PA6 GF30 | PA6 GF40 | PA6 GF50 |
|---|---|---|---|---|---|
| Tensile Strength (MPa, dry) | 70 – 85 | 110 – 130 | 160 – 190 | 180 – 200 | 200 – 220 |
| Módulo de flexión (MPa) | 2,500 – 3,000 | 4,500 – 5,500 | 8,000 – 10,000 | 10,500 – 12,000 | 13,000 – 15,000 |
| Alargamiento a la rotura (%) | 20 – 40 | 3 – 5 | 3 – 5 | 2 – 3 | 1.5 – 2.5 |
| Charpy Notched Impact (kJ/m², 23°C) | 5 – 8 | 8 – 12 | 10 – 15 | 12 – 16 | 13 – 17 |
| Densidad (g/cm³) | 1.13 – 1.15 | 1.20 – 1.23 | 1.35 – 1.38 | 1.44 – 1.48 | 1.55 – 1.58 |
| HDT/A, 1.8 MPa (°C) | 60 – 75 | 180 – 195 | 200 – 210 | 210 – 215 | 215 – 220 |
| Punto de fusión (°C) | 220 – 225 | 220 – 225 | 220 – 225 | 220 – 225 | 220 – 225 |
| Mold Shrinkage (flow, %) | 1.0 – 1.5 | 0.4 – 0.7 | 0.2 – 0.5 | 0.15 – 0.35 | 0.10 – 0.25 |
| Aplicaciones típicas | Non-structural clips, covers | Housings, brackets, medium stiffness | Engine covers, fan shrouds, power tool housings | High-stiffness frames, pump bodies | Metal replacement, extreme rigidity |
Selection guidance: PA6 GF30 is the most commonly specified glass-filled PA6 grade because it delivers the best stiffness-to-cost ratio for typical structural applications. Move to GF40 or GF50 only when the application demands stiffness approaching aluminum or when wall thickness is constrained. Stay with GF15 when flow into thin-wall features or impact toughness at low temperature matters more than maximum rigidity.
PA6 GF30 Commercial Grade Equivalents
| Supplier | PA6 GF30 Grade | Key Features |
|---|---|---|
| BASF | Ultramid B3WG6 / B3EG6 | General-purpose, heat-stabilized, excellent surface finish |
| DuPont | Zytel 73G30 HSL | Heat-stabilized, widely specified in automotive |
| LANXESS | Durethan BKV 30 H2.0 | Heat-aged, good flow for thin-wall parts |
| DSM / Envalior | Akulon K224-G6 | General-purpose, good chemical resistance |
| Domo / Solvay | Technyl C216 V30 | Widely available in Asia, good processability |
| EMS-Grivory | Grilon BG-30 | Good impact balance, suitable for structural parts |
| Radici | Radilon S RV300 | Easy flow, suitable for complex geometries |
| Ensinger | TECAMID 6 GF30 | Stock shapes and machined parts |
When substituting between PA6 GF30 suppliers, compare full datasheets in the same conditioned state (dry-as-molded vs 50% RH), verify mold shrinkage in both flow and transverse directions, and run a production-tool trial. Even nominally equivalent PA6 GF30 grades differ in fiber length retention, color stability, heat aging, and processing window.
Where PA6 GF30 Is Used
PA6 GF30 is commonly considered for structural parts that need higher stiffness and heat resistance than unfilled PA6. The selected commercial grade still has to meet the part’s impact, moisture, chemical, appearance, electrical and flame requirements.
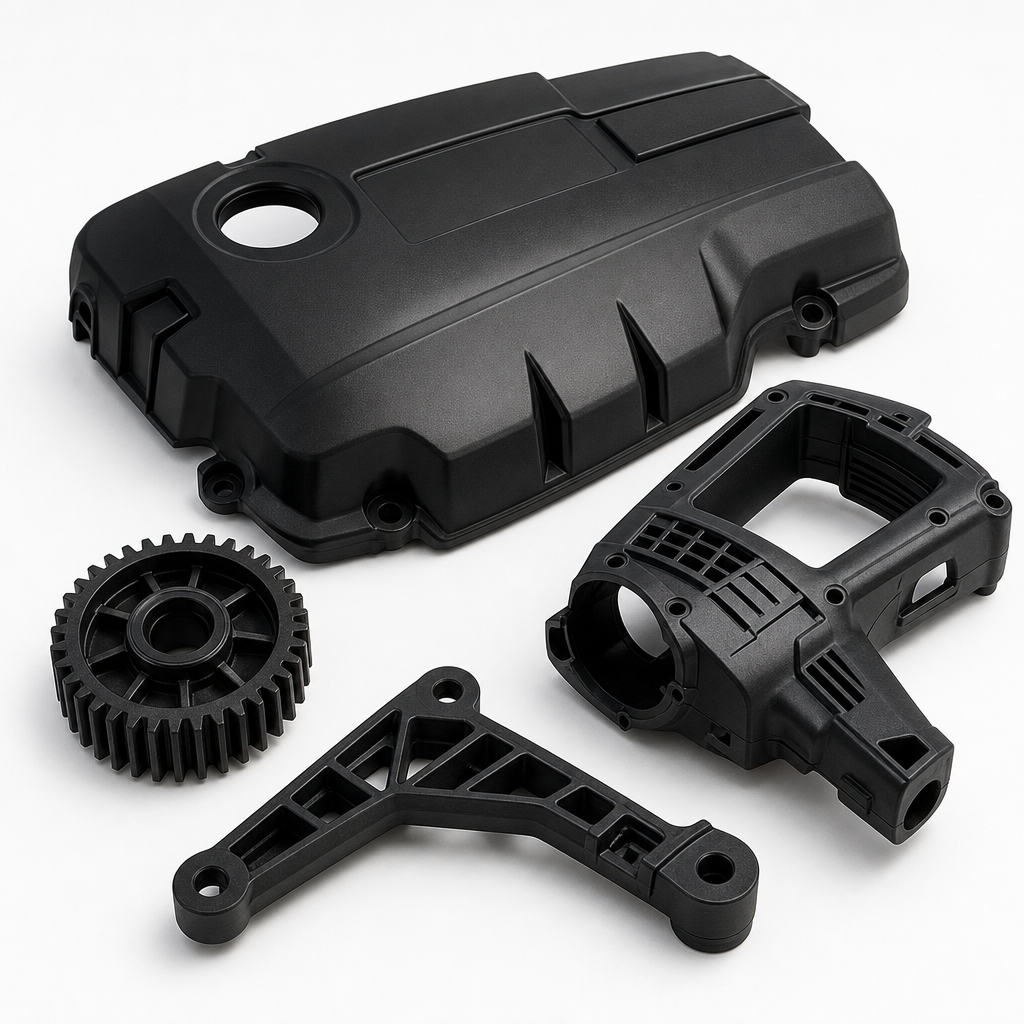
Fan shrouds, structural housings, brackets and selected under-hood components.
Pump bodies, impellers, machine housings and load-bearing supports.
Housings, connectors and supports when the grade meets the required electrical and flammability ratings.
Stiff housings, frames and mechanical components where fiber orientation and surface finish are controlled.
Acerca de nuestro suministro de plásticos técnicos
As an ISO 9001 certified engineering plastics manufacturer and exporter, we produce PA6 GF30 in heat-stabilized, impact-modified, UV-stabilized and color-matched variants. For the selected formulation, our technical team can provide the matching datasheet, batch-specific certificate of analysis and applicable RoHS, REACH or UL documentation. Send your target properties, annual volume and delivery destination to discuss a standard grade or custom formulation.
Need a PA6 GF30 datasheet for your application or a quotation for supply? Contact our team — specify your volume, delivery destination, and any special requirements (color, certification, impact modification). The current datasheet and quotation scope are confirmed for the selected grade and requirements.
Preguntas frecuentes
Is PA6 GF30 one standardized material?
No. PA6 GF30 identifies a PA6 material family with a nominal 30% glass-fiber level. The additive package, resin viscosity, fiber system and conditioning state vary by commercial grade, so compare the complete TDS and validate the molded part.
Is PA6 GF30 the same as PA66 GF30?
No. Both contain nominal 30% glass fiber, but PA6 and PA66 use different base polymers. They differ in melting and heat performance, moisture response, processing window and grade availability.
Is standard PA6 GF30 flame retardant?
Not automatically. A standard grade and a PA6 GF30 FR grade are separate selections. Confirm the exact UL 94 rating, specimen thickness and certification for the chosen commercial grade.
¿Cuáles son las propiedades clave que hay que comprobar en la ficha técnica del PA6-GF30?
Check tensile strength, flexural modulus, the named impact method, HDT test load, density, shrinkage and specimen conditioning. As a named example, WHG30A lists 165 MPa tensile strength (ISO 527-2), 6,000 MPa flexural modulus (ISO 178) and 175°C HDT (ISO 75-2/B, 0.45 MPa). Do not treat the cross-supplier ranges as guarantees for WHG30A.
¿Por qué varían los valores de resistencia que figuran en la ficha técnica del PA6-GF30 según el proveedor?
Glass fiber type and length, coupling system, base resin, additives and conditioning can change the result. Compare values measured by the same method and conditioning state; there is no universal percentage allowance that makes two grades equivalent.
¿Cómo debo interpretar los valores de la ficha técnica del PA6-GF30 para mi diseño?
Choose dry or conditioned data to match the part’s actual service environment, then validate critical dimensions and loads on molded samples. The WHG30A PDF does not state conditioning. Set design margins from the part loads, environment and failure consequences; the datasheet alone does not define a universal safety factor.
¿Qué parámetros de procesamiento debe incluir una buena ficha técnica del PA6-GF30?
Check the selected grade’s drying, melt and mold temperatures, moisture limit and injection settings. The WHG30A one-page PDF provides property data but no processing window; the parameters above are starting points for trials, not guaranteed WHG30A settings.
Technical Review and Data Sources
Technical author and reviewer: WanHan Technical Team
Last Technical Review: September 28, 2026
- WanHan PA6 WHG30A Technical Data Sheet is the source for the named WHG30A values on this page.
- ISO 1183, ISO 527-2, ISO 178, ISO 179, ISO 75-2/B and ISO 2577 are cited as printed in that TDS; noted method inconsistencies must be confirmed before approval.
- Cross-supplier values are reference ranges. Exact properties depend on grade, test method and conditioning; use the current grade TDS and representative testing for qualification.