Why Finish Nylon Surfaces?
Nylon parts often emerge from the mold or CNC machine with perfectly functional geometry—but the surface may not meet the final application’s aesthetic, functional, or branding requirements. Surface finishing transforms raw nylon from a matte, slightly greasy-feeling engineering material into a component that looks premium, resists environmental attack, or communicates critical information through marking and labeling.
The challenge with nylon is its low surface energy—typically 36–42 mN/m, compared to 46+ mN/m for metals and other plastics. This means paints, inks, and adhesives don’t wet the surface naturally. Every finishing process for nylon must begin with surface preparation to raise the surface energy and create anchor points for the subsequent coating or treatment.
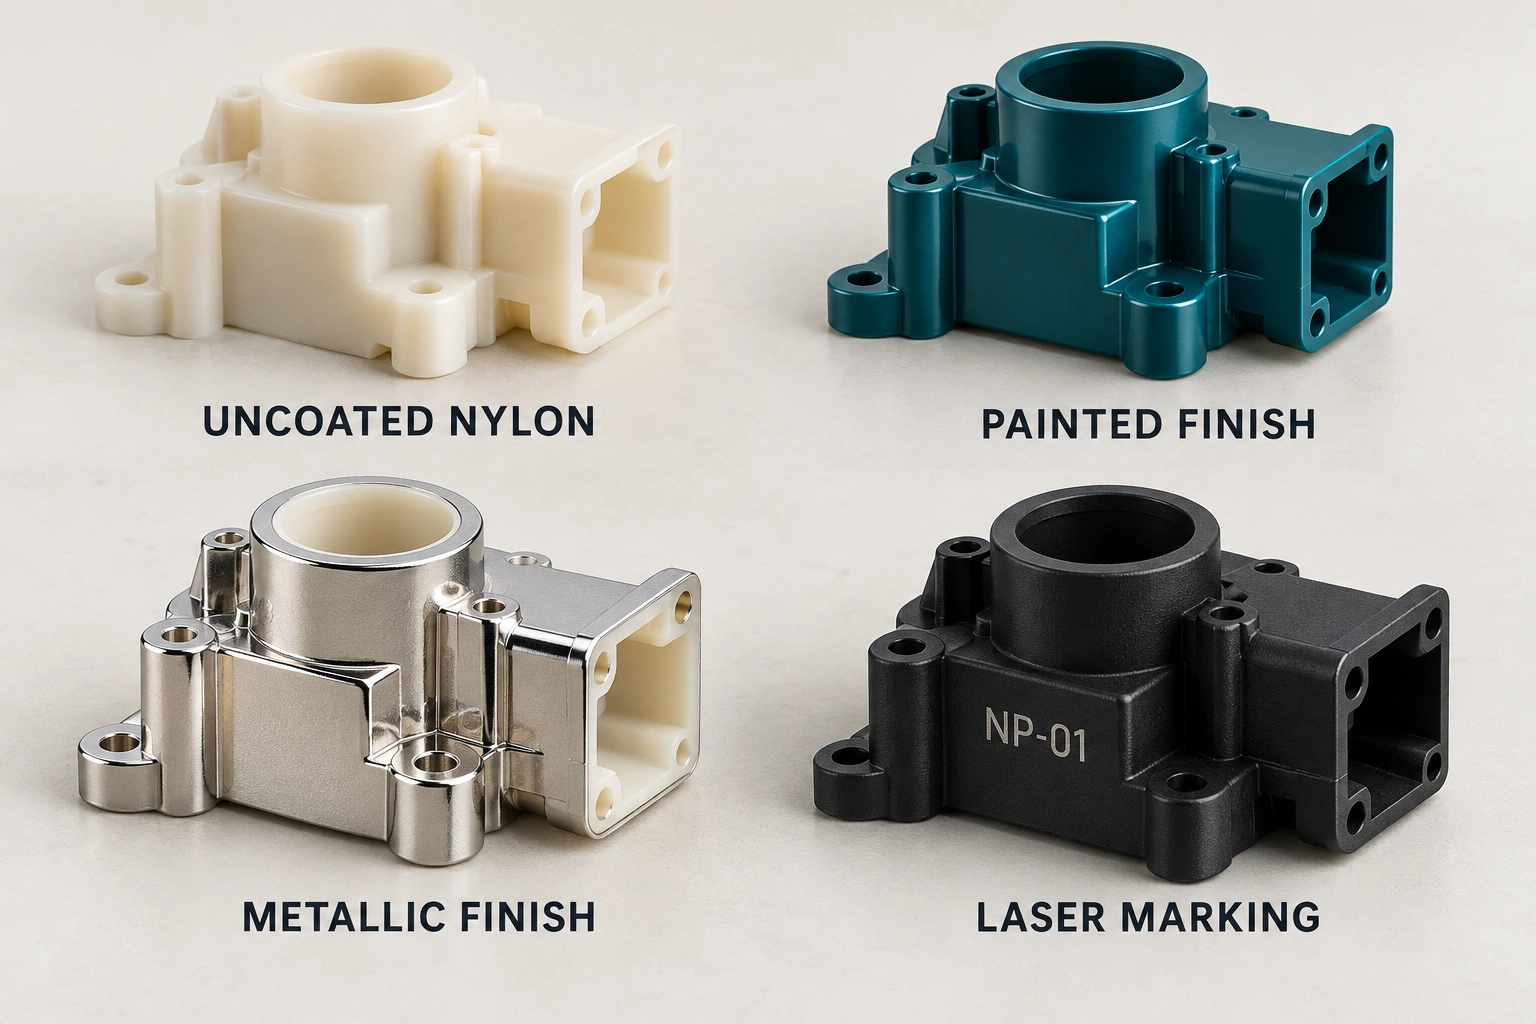
When the substrate grade is still open, start with the engineering plastics selection guide before agreeing the finish.
Surface Preparation: The Non-Negotiable First Step
All nylon finishing processes require one of these preparation methods:
| Método | Surface Energy After | Durabilidad | Lo mejor para |
|---|---|---|---|
| Flame treatment | 50–60 mN/m | Hours–days | High-volume in-line painting; simple geometries |
| Plasma treatment | 55–72 mN/m | Hours–days | Complex 3D parts; selective treatment possible |
| Chemical etching | Indefinido | Indefinido | Plating (creates micro-roughness for mechanical anchoring) |
| Primer application | N/A (chemical bond) | Indefinido | Painting; specialized nylon primers available |
| Mechanical abrasion | 42–48 mN/m | Indefinido | Low-cost option; adequate for non-critical bonds |
For molded nylon substrates, the nylon injection molding guide covers the material preparation and molding stage before finishing.
Painting Nylon
Painting nylon requires a three-layer system for reliable adhesion and durability:
- Primer: A nylon-specific adhesion promoter (typically chlorinated polyolefin or acrylic-modified) applied at 5–10 μm dry film thickness. This is the critical layer—standard primers will not bond to nylon.
- Base coat: The color layer, applied at 15–25 μm. Polyurethane and acrylic lacquers are most common.
- Clear coat (optional): 20–40 μm of UV-resistant clear for exterior automotive and consumer applications.
For best results, paint within 2 hours of surface activation treatment. If parts must be stored, protect from dust and humidity, and re-treat before painting if stored more than 8 hours.
Consulta el surface finishing service scope when specifying the substrate, appearance reference and areas to finish in your quotation request.
Electroplating Nylon
Nylon can be electroplated with copper, nickel, and chromium to create a true metallic surface with the weight and cost advantages of a plastic substrate. The process is more demanding than plating ABS—the standard platable plastic—but well-established for nylon 6 and nylon 66.
The plating process:
- Etch: Chromic acid/sulfuric acid mixture creates micropores on the nylon surface
- Neutralize & catalyze: Palladium-tin colloidal solution deposits catalytic sites
- Electroless nickel or copper: Deposition of a conductive layer (0.5–1.0 μm)
- Electrolytic plating: Build-up of copper (15–25 μm), nickel (8–15 μm), and chromium (0.25–0.5 μm)
Laser Marking Nylon
Laser marking has become the preferred method for adding permanent text, barcodes, logos, and UDI (Unique Device Identification) codes to nylon parts. The process creates a high-contrast mark without inks, labels, or physical contact.
Key process parameters:
- Fiber lasers (1064 nm): Best for creating dark marks on light-colored nylon through carbonization at the surface
- CO₂ lasers (10.6 μm): Create lighter marks through controlled surface melting; less common for nylon
- UV lasers (355 nm): “Cold marking” with minimal thermal damage; excellent for medical device marking where surface integrity is critical
- Laser-sensitive additives: 0.5–2% of metal oxide or mica-based additives can dramatically improve contrast and marking speed
Other Finishing Options
- Tampografía: Silicone pad transfers ink from an etched plate to the nylon surface. Excellent for small logos and text on curved surfaces. Requires flame or plasma pre-treatment.
- Estampado en caliente: Heated die transfers foil to the surface under pressure. Creates a premium metallic or colored finish without solvents. Good for logos and decorative bands.
- Hydrographic printing (water transfer): Patterned film floats on water and transfers to the part as it’s dipped. Can apply wood grain, carbon fiber, camouflage, and custom patterns. Requires full-surface primer and clear coat.
- Vibratory finishing: For machined nylon parts, ceramic or plastic media in a vibratory bowl removes tool marks and creates a uniform matte finish.
Preguntas frecuentes
Can a molded or machined nylon part be painted?
Painting is a possible finishing route, but preparation and the coating system must be selected for the actual nylon grade and part condition. Identify visible surfaces, color, gloss, cleaners and service exposure; approve representative coated parts and an agreed adhesion check before repeat production.
Does every nylon grade accept the same metallic finish?
No finish should be assumed suitable from the PA6 or PA66 name alone. Reinforcement, additives, substrate condition, geometry and the proposed process affect the review. Define masking, mating fits and the required appearance and durability tests with the finishing scope.
What should be specified for laser marking on nylon parts?
Provide the artwork or identifier, marked area, exact grade and color, required contrast and any reading or traceability requirement. Approve the mark on representative parts; neither a light mark nor a dark mark is guaranteed for every nylon formulation.
What affects the quotation for finished nylon components?
Quantity, part geometry, exact grade, preparation, masking, chosen finish, artwork, sample trials, inspection and packaging affect scope. State whether you need finishing on supplied parts or manufacture and finish together so quotes include the same responsibilities.
Lecturas relacionadas
Request a Nylon Surface Finish Review
For nylon surface finishing on molded or machined components, send the part drawing and the appearance or marking requirement. Nylon Plastic can review the nylon grade, preparation, finish, protected surfaces and sample acceptance alongside the part manufacturing scope.
Qué hay que incluir y acordar antes de elaborar el presupuesto
- Provide exact nylon grade, reinforcement, color, molded or machined substrate, drawing revision, sample quantity, annual demand, destination and timing.
- Identify painted, metallic, printed or laser-marked surfaces, color and gloss reference, texture, artwork and viewing conditions; mark bores, threads, seals and bond areas that must be protected.
- State cleaners, chemicals, wear, outdoor exposure, service temperature and any regulatory requirements. Define adhesion, appearance, abrasion or marking checks appropriate to the actual component.
- Agree preparation and handling, finish thickness where relevant, masking, inspection, approved samples, packaging and who accepts each result.
- ✅ Más de 300 máquinas de moldeo por inyección de 50T a 2000T
- ✅ Más de 10.000 piezas al día capacidad de producción
- ✅ Precisión de ±0,02 mm tolerancia en todos los materiales
- ✅ MOQ sólo 1 pieza para prototipos; escalable a millones
- ✅ 24 horas de cotización, Plazos de entrega de 3 a 15 días
- ✅ Sistema de gestión de la calidad con certificación ISO 9001
Separate component manufacture, surface preparation, finishing, sample trials and inspection in the quotation. Approve representative parts of the selected grade before recurring orders; a finish name alone does not define durability or appearance.